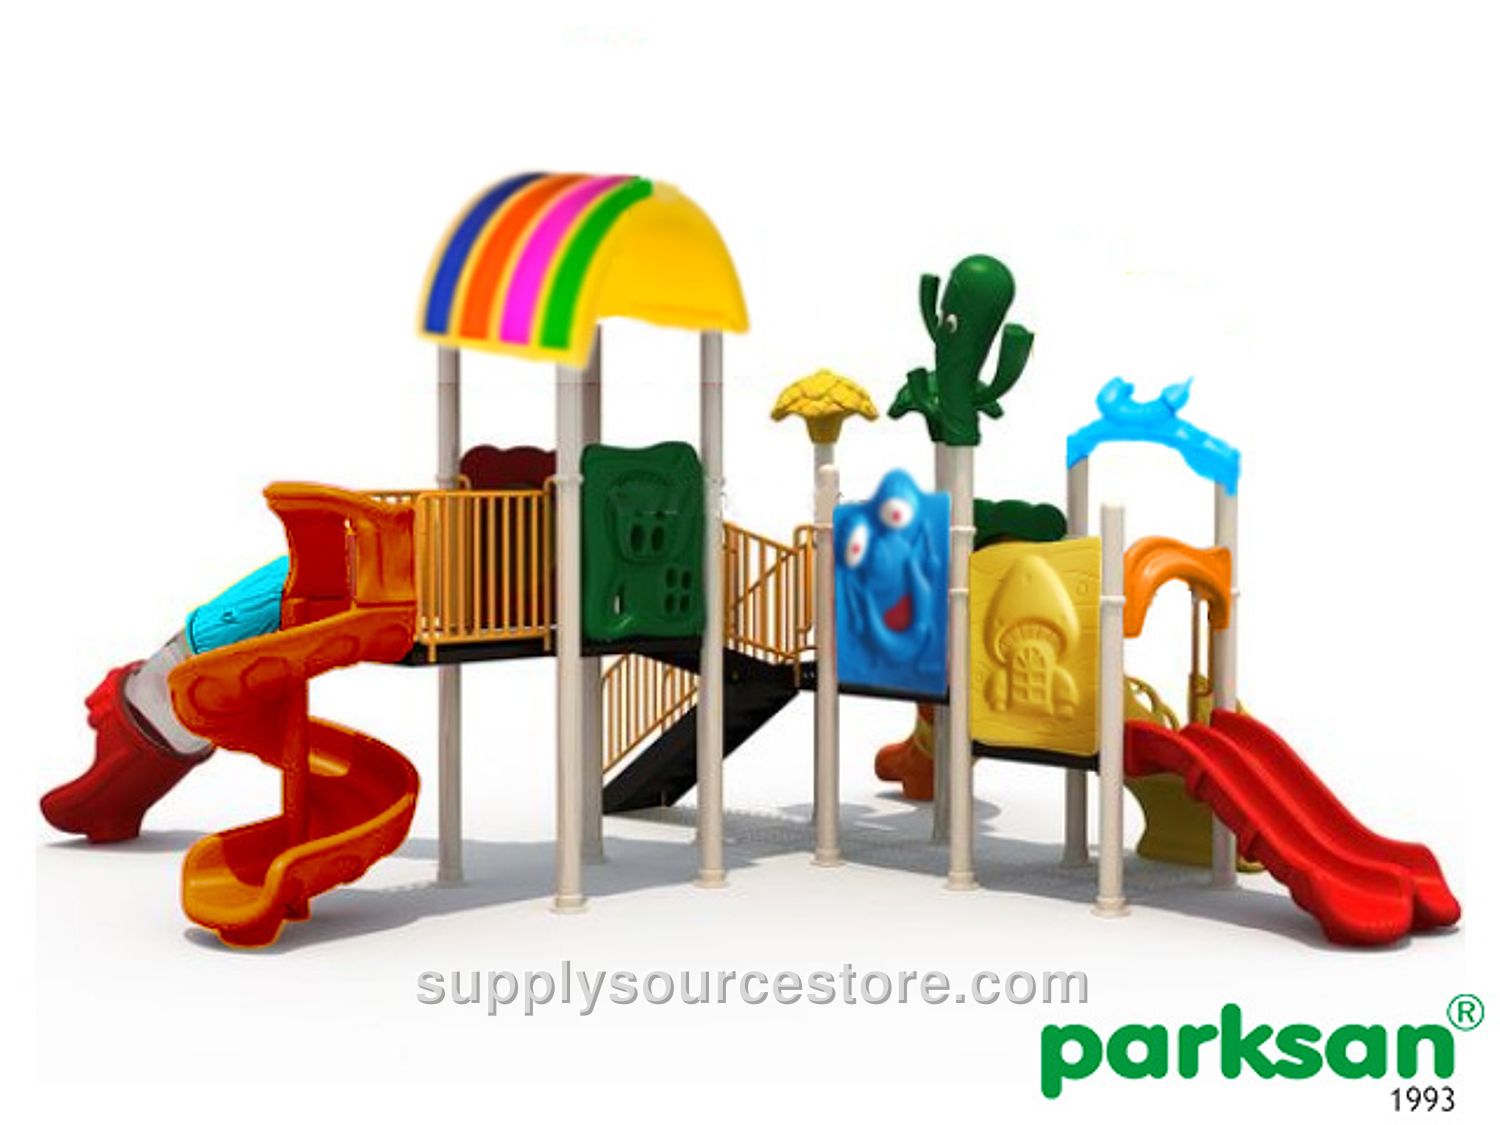
Rainbow Series Playground
Price on request
SKU: S27-PS-0050508
Product spare parts. 116x116 composite square platform – 3 pcs. Composite stairs – 3 pcs. Metal stair rail – 3 pcs. Metal spiral slide extension – 1 pc. Metal spiral slide extension rail – 1 pc. Polyethylene play area barrier – 5 pcs. H:100 cm (39.4 in) straight slide – 1 pc. H:100 cm (39.4 in) double straight slide – 1 pc. H:200 cm (78.7 in) spiral slide – 1 pc. H:200 cm (78.7 in) tube slide – 1 pc. Composite intermediate stair – 1 pc. Polyethylene slide entrance – 3 pcs. Rainbow roof – 1 pc. Polyethylene leaf figure – 2 pcs. Polyethylene cactus figure – 1 pc. H:100 cm (39.4 in) tower pipe – 6 pcs. H:150 cm (59.1 in) tower pipe – 4 pcs. Polyethylene products are a thermoplastic used in various applications. Low‑density linear polyethylene (LLDPE) is semi‑permeable, pliable and very durable, offering low cost and high resistance, making it popular in industry. It is classified based on density and chemical properties. Mechanical properties depend on molecular weight, crystal structure and branching type. While properties vary, they generally provide good resistance to outdoor conditions and moisture, flexibility, low mechanical strength and excellent chemical resistance. Polyethylene is used to manufacture slides, stairs, railings, barriers, accessories, roofs, etc. To prevent color fading, masterbatch pigments used for coloring must have a light fastness rating of 6 or higher. The product’s wall thickness must be at least 6 mm (0.2 in) for areas subject to pressure or friction, and at least 4 mm (0.2 in) for non‑load‑bearing barrier or shade components. Thickness must be uniform, with a dimensional tolerance of ±5%. Carrier construction: Steel tubes with a minimum 114 mm (4.5 in) diameter and at least 2 mm (0.1 in) wall thickness are cold‑formed according to TS EN 10219‑2, TS‑6476, DIN 2394 standards and welded by high‑frequency welding. They are sandblasted and coated with a polyester‑based electrostatic powder paint. Electrostatic powder coating: All metal parts are sandblasted to remove oil, dirt and rust, creating a porous surface for better paint adhesion. Fine steel beads are sprayed with compressed air to open pores and clean the surface. After sandblasting, parts are coated with polyester‑based electrostatic paint and cured in a 200‑220 °C oven for 20 minutes. Subsequently, parts undergo a 10‑minute 70 °C dip in a 5 % degreasing bath, followed by a 15‑minute 50 °C dip in a 1 % acid pickling bath, rinsing, drying, and final curing at 180‑200 °C for 20‑30 minutes. Weld seams are fully painted to prevent rust.