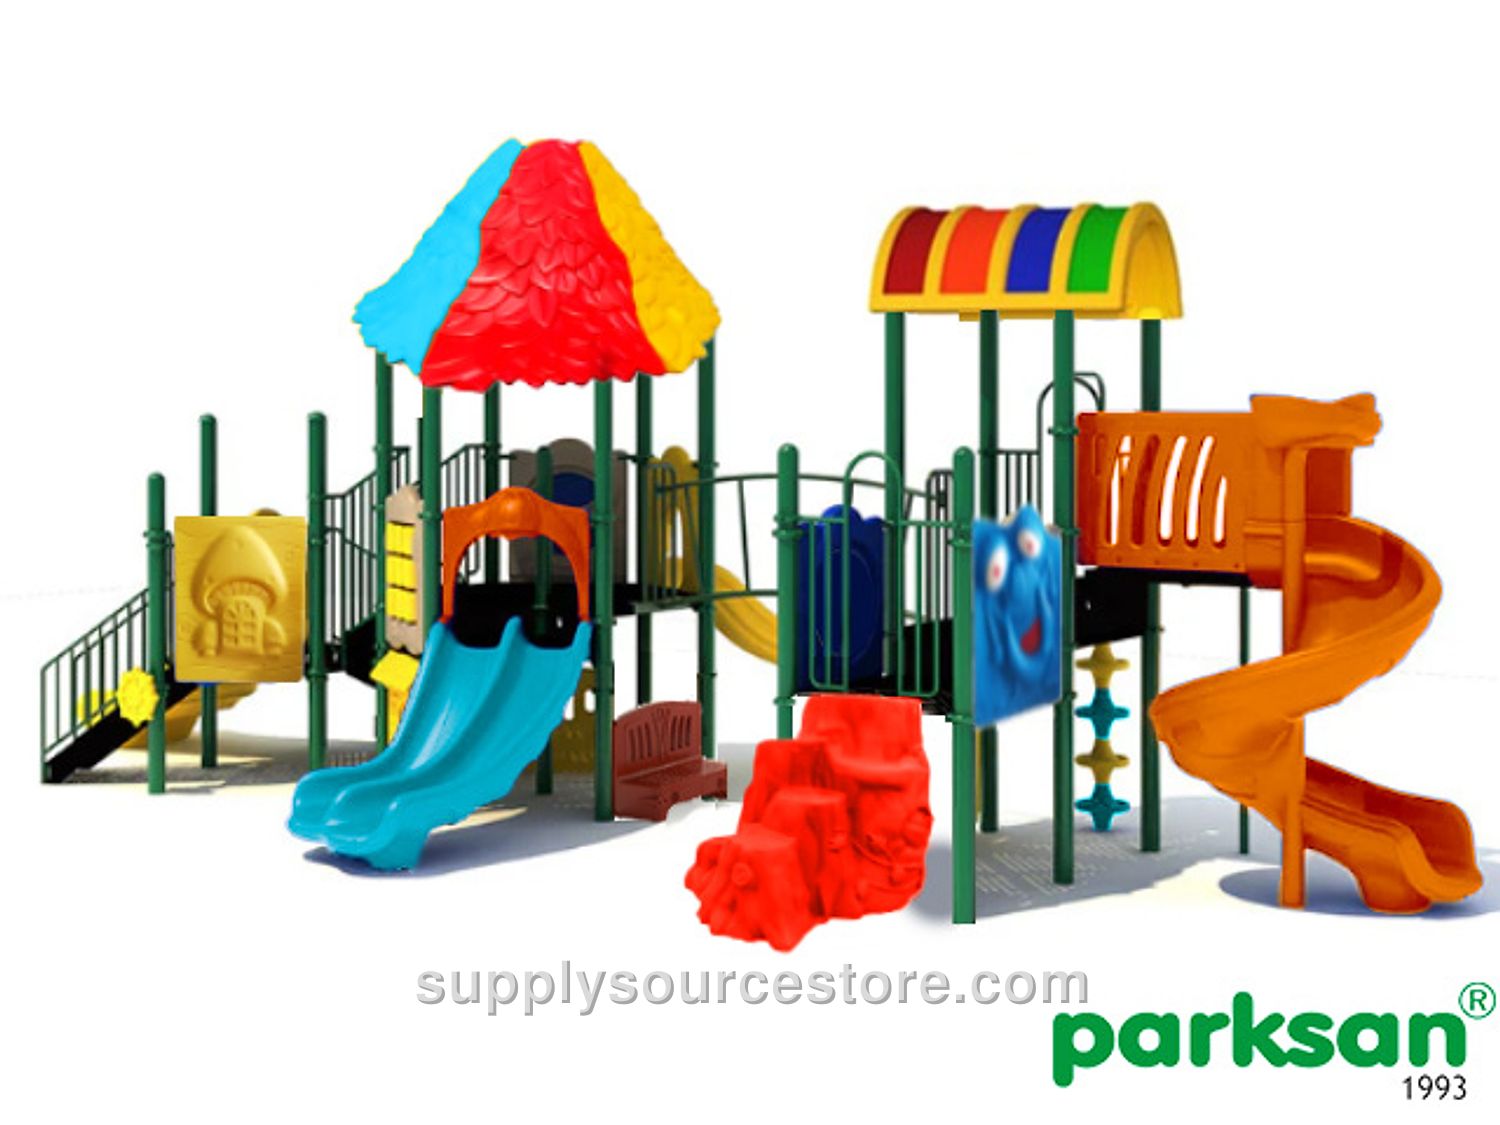
Rainbow Series Playground
Price on request
SKU: SS-012558
Spare Parts - 116x116 composite square platform – 3 pcs - 116x116 composite triangular platform – 6 pcs - Composite staircase – 1 pc - Metal railing – 2 pcs - Composite intermediate staircase – 3 pcs - Polyethylene lounge barrier – 7 pcs - H:150 UFO climbing element – 1 pc - Polyethylene seating panel – 1 pc - Polyethylene slide entrance – 3 pcs - Rainbow roof – 1 pc - Polyethylene six‑leaf roof – 1 pc - H:100 cm (39.4 in) straight slide – 1 pc - H:150 cm (59.1 in) double right‑inclined slide – 1 pc - H:150 cm (59.1 in) wavy slide – 1 pc - H:200 cm (78.7 in) spiral slide – 1 pc - Metal spiral slide extension – 1 pc - Metal spiral slide extension railing – 1 pc - Metal climbing entrance – 1 pc - Polyethylene climbing log – 1 pc - H:100 cm (39.4 in) open‑top tower tube – 6 pcs - H:150 cm (59.1 in) roofed tower tube – 6 pcs - H:200 cm (78.7 in) roofed tower tube – 4 pcs Polyethylene Products Low‑density linear polyethylene (LLDPE) is a thermoplastic used in various products. It is a semi‑transparent, pliable, and highly durable polymer. Its low cost and high resistance make it popular in industry. Polyethylene grades are classified based on density and chemical properties. Mechanical properties depend on molecular weight, crystalline structure, and branching type. Although properties vary, it generally offers good resistance to outdoor conditions and moisture, flexibility, low mechanical strength, and excellent chemical resistance. Polyethylene components are used to manufacture slides, stairs, railings, barriers, accessories, roofs, etc. To prevent color fading, masterbatch pigments used for coloring must have a lightfastness rating of 6 or higher. The material thickness must be at least 6 mm (0.2 in) for parts exposed to pressure or friction, and at least 4 mm (0.2 in) for barrier or shading components that are not pressure‑exposed. Thickness uniformity must be maintained, and dimensional tolerance is ±5 %. Electrostatic Powder Coating All metal parts are prepared for painting by bead blasting to remove oil, dirt, and rust, creating a porous surface for better paint adhesion. After blasting, a fine metal shot is propelled with compressed air to further open pores. The components are then cleaned in a 70 °C, 5 % degreasing bath for 10 minutes, followed by a 50 °C, 1 % acid bath for 15 minutes, rinsed, and dried. A polyester‑based electrostatic powder coating is applied, and the parts are cured in a 200‑220 °C oven for 20 minutes. After fabrication, welds are treated to prevent corrosion and the entire assembly is painted as a single piece.