Economic Series Playground · SS-012548
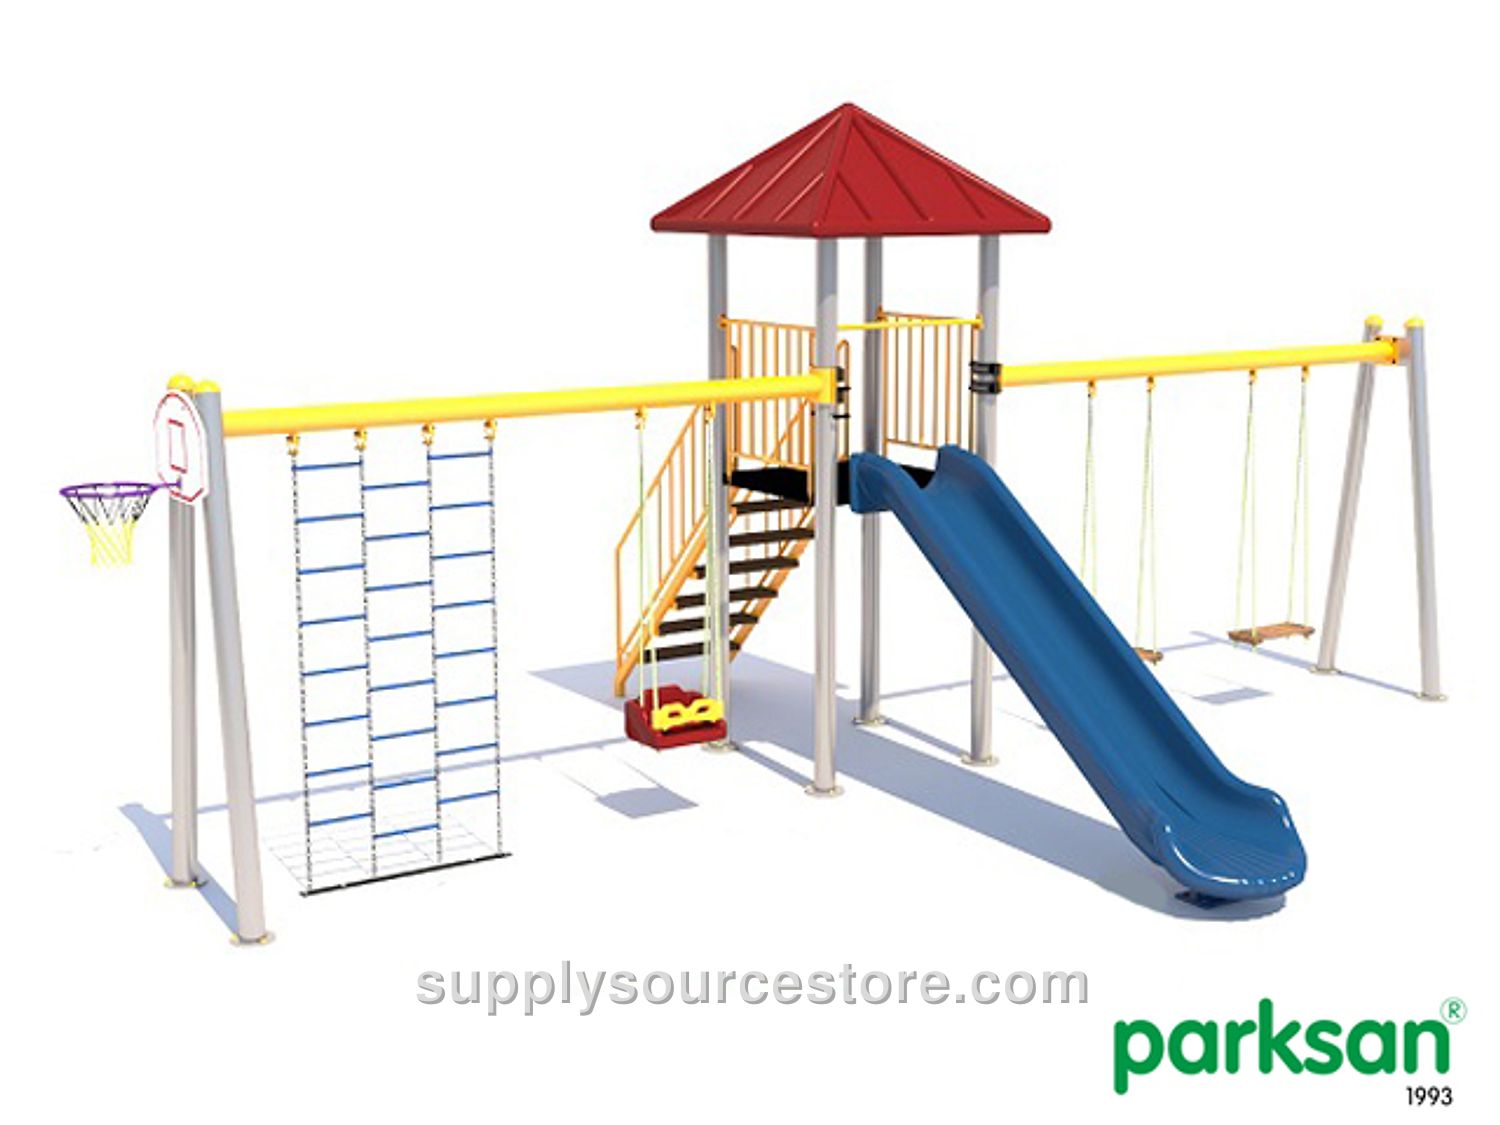
Price on request
SKU: SS-012548
Product Technical Features Seating Area: 530 × 730 cm (209 x 287 in) Safety Area: 830 × 1030 cm (327 x 406 in) Slide Connection Height: 150 cm (59.1 in) User Capacity: 3 User Age Group: 3+ Carrier Construction The carrier structure will be fabricated from cold‑formed steel tubes that meet TS EN 10219‑2, TS‑6476, DIN 2394 standards, with a minimum diameter of 89 mm (3.5 in) and a wall thickness of at least 2.5 mm (0.1 in). Tubes will be welded by high‑frequency welding and produced within the standard tolerances, dimensions, and cross‑section ranges. After sandblasting, the tubes are painted with a polyester‑based electrostatic powder‑coat in a furnace. The upper ends of these tubes are sealed with polyethylene caps fastened by at least two aluminum rivets, each rivet forming a half‑sphere to prevent water, moisture, and foreign matter from entering. Vertical and horizontal sandblasted tubes (minimum 89 mm (3.5 in) diameter) are joined at right angles using aluminum‑cast or injection‑molded polyamide connection elements. The lower sections of the carrier tubes are welded to steel plate flanges measuring at least 150 × 150 × 5 mm (5.9 x 5.9 x 0.2 in). When the installation surface is a hard ground, the carrier tubes are anchored to the ground with steel dowels (minimum 8 × 75 mm (0.3 x 3 in)) inserted through 10 mm (0.4 in) holes in the plate flanges. For soil installations, an anchorage system consists of four galvanized M10 × 40 screws welded to a 150 × 150 × 5 mm (5.9 x 5.9 x 0.2 in) plate flange, attached to a sandblasted tube of at least 200 mm (7.9 in) height, 89 mm (3.5 in) diameter, and 2.5 mm (0.1 in) wall thickness. All carrier tubes are single pieces; no additional tubes, welds, or seams are permitted. Platforms, guardrails, or clamps are not welded directly to the carrier tubes. However, when mounting plastic‑covered or steel platforms, flanges with a minimum 5 mm (0.2 in) wall thickness may be welded to match the platform corners and bolt holes. CTP (Glass‑Fiber‑Reinforced Polyester) Products CTP stands for "Cam Elyaf Takviyeli Polyester" (Glass‑Fiber‑Reinforced Polyester). CTP is used for slides, stairs, guardrails, barriers, accessories, roofs, etc. The material is a composite of unsaturated polyester reinforced with glass fibers, offering increased mechanical strength while remaining lightweight. It is resistant to climatic variations, temperature changes, chlorine‑containing water, and all typical chemicals, and it does not become conductive. The glass fibers are woven into a fine, flexible fabric that is placed in a mold, combined with polyester resin and a catalyst, and then layered and cured. The resulting material is strong, lightweight, smooth, and can be sanded and painted. A performance gelcoat containing an isophthalic/NPG‑based acrylic modifier provides superior resistance to heat up to 215 °C, fatigue, cracking, yellowing, fading, and gloss loss. Two coats (0.80 µm each) are applied, yielding a total film thickness of 5 mm (0.2 in) with a coating weight of 450 g/m² for the top coat and 600 g/m² for the base coat, using CE 92 N8 polyester for high mechanical resistance. No additional coloring is applied. Polyethylene Products Low‑density linear polyethylene (LLDPE) is a thermoplastic used in many components such as slides, stairs, guardrails, barriers, accessories, and roofs. It is semi‑permeable, flexible, and highly durable, offering low cost and high resistance to chemicals and moisture. Mechanical properties depend on molecular weight, crystallinity, and branching. All polyethylene parts intended for slides, stairs, guardrails, barriers, and accessories meet a light‑fastness value of 6 or higher. Wall thickness for load‑bearing areas must be at least 6 mm (0.2 in), while non‑load‑bearing barriers and shade structures require a minimum of 4 mm (0.2 in). Thickness tolerances are ±5 %. Electrostatic Powder‑Coat Painting All metallic components are prepared by sandblasting to remove oil, dirt, and rust, creating a porous surface that improves powder‑coat adhesion. The powder is then applied using a fine‑particle stream propelled by compressed air, ensuring an even coating that adheres firmly to the cleaned metal surfaces. All metal parts are fabricated according to the above processes.