Children Playground (Afacan Series)
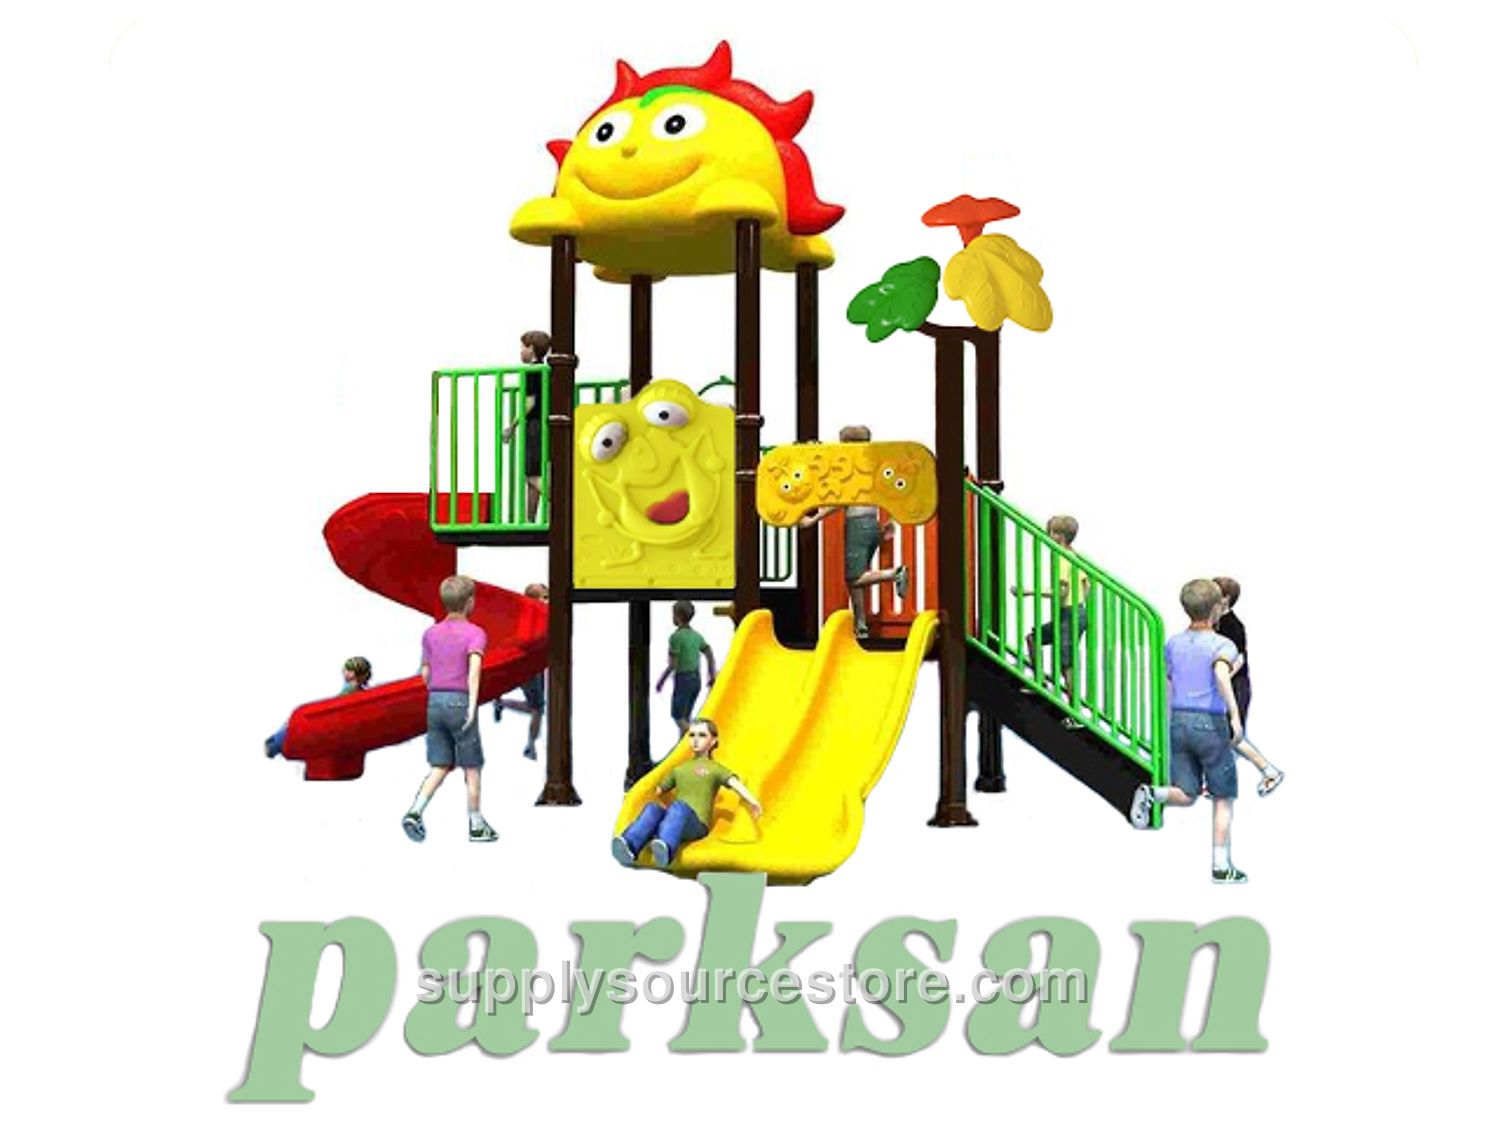
Price on request
SKU: PS-0050112
POLYETHYLENE PRODUCTS Low-density or linear low-density polyethylene (LLDPE) is a thermoplastic used in various products. It is a semi‑permeable, softening and highly durable polymer that is favored in industry due to its low cost and high resistance. Based on polyethylene density and chemical properties, it is classified into several categories. Mechanical properties depend on molecular weight, crystal structure and branching type. While properties vary by grade, general characteristics include good resistance to outdoor conditions and moisture, flexibility, low mechanical strength, and excellent chemical resistance. Polyethylene products are used to manufacture slides, stairs, railings, barriers, accessories, roofing, etc. To prevent color fading, masterbatch pigments used to color polyethylene must have a light fastness rating of 6 or higher. Wall thickness must be a minimum of 6 mm (0.2 in) for areas exposed to pressure and friction, and a minimum of 4 mm (0.2 in) for barrier and shading items not subject to pressure. Material must be evenly distributed to achieve uniform thickness. Product wall thickness and dimensional tolerance are ±5 %. CARRIER CONSTRUCTION Steel tubes with a minimum diameter of 114 mm (4.5 in) and a minimum wall thickness of 2 mm (0.1 in), conforming to TS EN 10219‑2, TS‑6476, DIN 2394, will be cold‑formed, welded by high‑frequency welding, and produced within standard tolerances, dimensions and cross‑section ranges. These carrier tubes will be sandblasted and then painted with a polyester‑based electrostatic powder coating. ELECTROSTATIC POWDER COATING All metal parts will be sandblasted to remove oil, dirt and rust, creating a porous surface for better paint adhesion. Fine steel beads will be shot with compressed air to open pores and eliminate contaminants before coating. After fabrication, metal components will be coated with a polyester‑based electrostatic paint and cured in a 200‑220 °C oven for 20 minutes. Subsequently, each metal part will be rinsed in a 10‑minute, 70 °C, 5 % degreasing bath, followed by a 15‑minute, 50 °C, 1 % iron pick‑ling bath, then rinsed and dried. Finally, the material will be coated with a durable outdoor polyester powder paint and baked in a 180‑200 °C oven for 20‑30 minutes. Weld seams will be fully painted after welding to prevent corrosion.