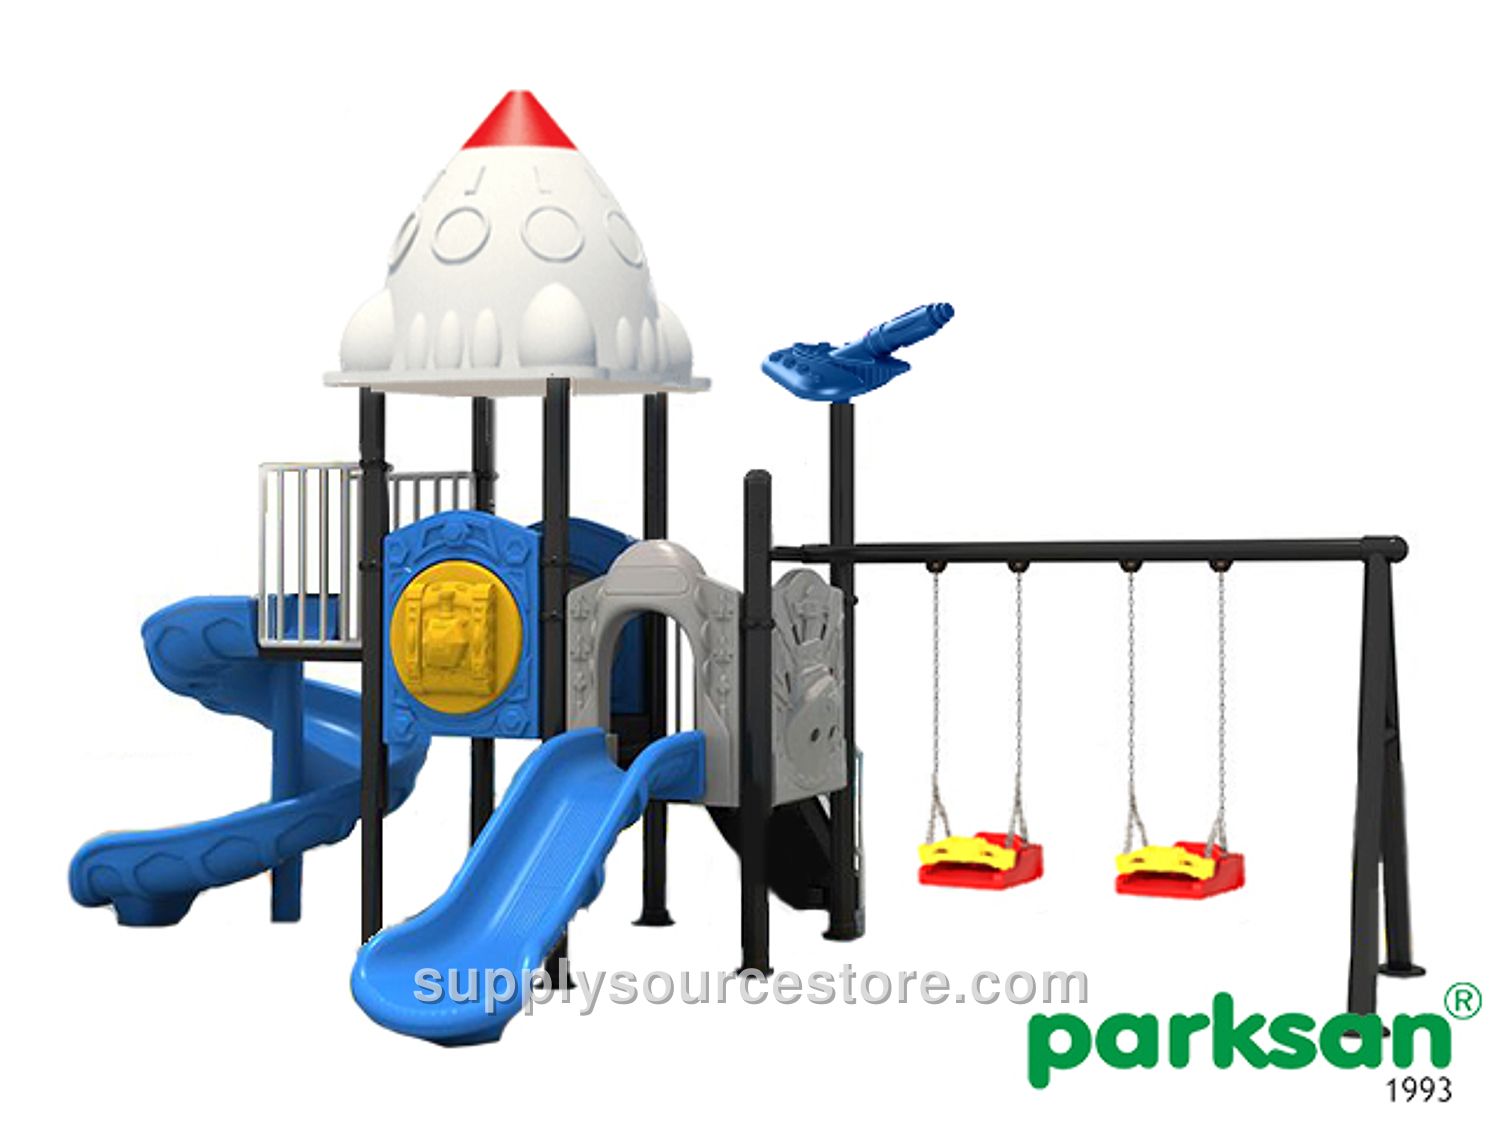
Children's Playground (Afacan Series) · SS-012291
Price on request
SKU: SS-012291
Polyethylene Products Low or medium density linear polyethylene (LLDPE – Linear Low Density Polyethylene) is a thermoplastic used in a variety of products. It is a semi‑permeable, pliable, and highly durable polymer that is favored in industry for its low cost and high resistance. Based on density and chemical properties, polyethylene is classified into several categories. Its mechanical properties depend on molecular weight, crystalline structure, and branching type. While properties vary by grade, common characteristics include good resistance to outdoor conditions and moisture, flexibility, low mechanical strength, and excellent chemical resistance. Polyethylene is used to manufacture slides, stairs, railings, barriers, accessories, roofs, and more. To prevent color fading, masterbatch pigments used for coloring polyethylene must have a light fastness rating of 6 or higher. Wall thickness must be at least 6 mm (0.2 in) for sections exposed to pressure or friction, and at least 4 mm (0.2 in) for barriers or shade structures that are not load‑bearing. Material distribution must be uniform, creating consistent thickness. Wall thickness and dimensional tolerances are limited to ±5 %. Carrier Construction The carrier structure is made from steel tubes with a minimum diameter of 114 mm (4.5 in) and a minimum wall thickness of 2 mm (0.1 in), cold‑formed to TS EN 10219‑2, TS‑6476, DIN 2394 standards and welded by high‑frequency welding. Tubes are then coated with polyester‑based electrostatic powder paint applied after sandblasting. Electrostatic Powder Paint Process All metal components are sandblasted to remove oil, dirt, and rust, creating a porous surface for optimal paint adhesion. Fine steel beads are then sprayed with pressurized air to open micro‑pores and clean the metal surface. After fabrication, the components are coated with polyester‑based electrostatic paint and cured in a 200–220 °C oven for 20 minutes. Subsequent finishing steps include a 10‑minute 70 °C dip in a 5 % oil‑removal bath, followed by a 15‑minute 50 °C dip in a 1 % iron‑pickling bath, rinsing, and drying. Finally, the entire assembly is powder‑coated with a weather‑resistant polyester paint and baked at 180–200 °C for 20–30 minutes. Weld seams are fully painted to prevent corrosion.