Next Generation Playground Play Set · SS-012082
Price on request
SKU: SS-012082
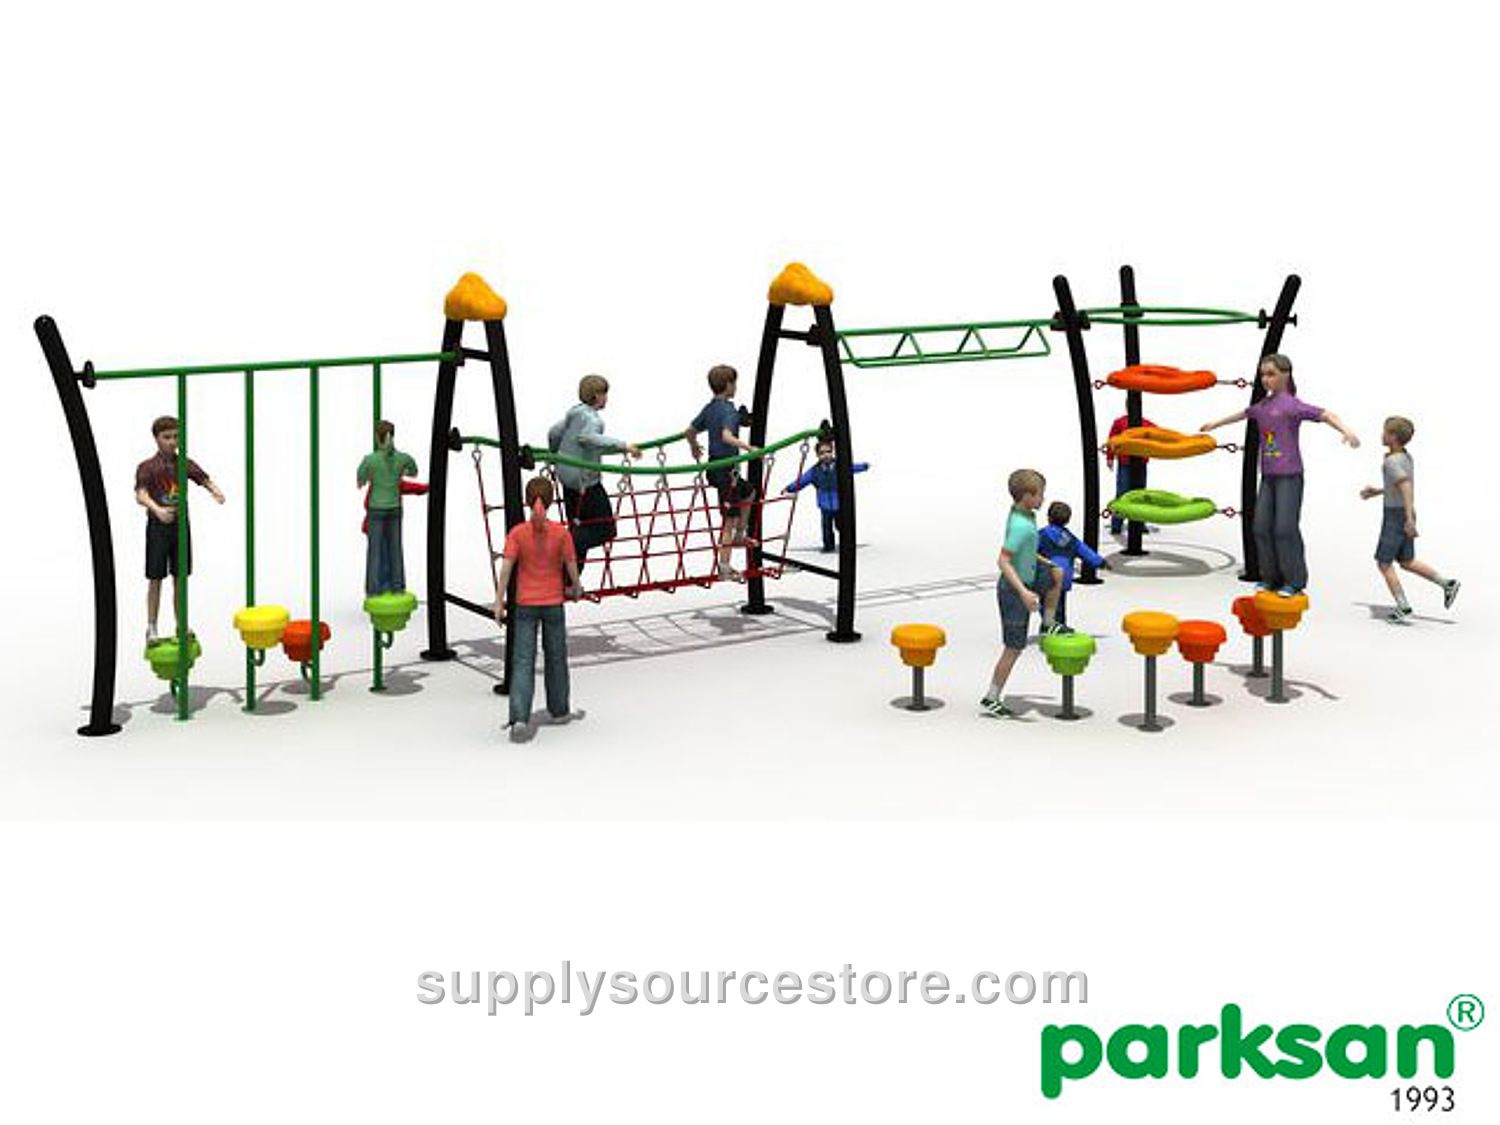
Product Technical Specifications Usage Area: 438×1325 cm (172 x 522 in) Safe Area: 442×1330 cm (174 x 524 in) User Age: 5+ years Capacity: 10‑16 persons Material: LLDPE Metal parts: Galvanized steel Fastening elements and clamps: Aluminum alloy Nylon net: consists of six steel cables with a total diameter of 16 mm (0.6 in). Function: Climbing activities that strengthen arms and legs, coordinate the body and improve balance. Spare Parts H:245cm (96.5 in) Single‑row Wavy Bridge – 1 ADET H:245cm (96.5 in) Single Straight Tepegöz Parallel Bar Climbing Element – 1 ADET H:245cm (96.5 in) Single Straight Inclined Wavy Bridge – 1 ADET H:60cm (23.6 in) Single Wavy Stone – 6 ADET H:245cm (96.5 in) Seamless Passage Climbing Element – 1 ADET Polyethylene Products Low‑density linear polyethylene (LLDPE) is a thermoplastic used in various products. It is a semi‑permeable, softening, and highly durable polymer that is inexpensive and highly resistant, making it popular in industry. Polyethylene density and chemical properties determine its classification into various categories. Its mechanical properties depend on molecular weight, crystal structure, and branching type. Although properties vary by grade, it generally offers good resistance to outdoor conditions and moisture, flexibility, low mechanical strength, and excellent chemical resistance. Polyethylene is used for slides, stairs, railings, barriers, accessories, roofing, etc. To prevent color fading, masterbatch pigments used for coloring polyethylene must have a light fastness rating of 6 or higher. The product’s wall thickness must be at least 6 mm (0.2 in) in areas exposed to pressure and friction, and at least 4 mm (0.2 in) for barriers and shade structures not exposed to pressure. Material distribution should be uniform to achieve consistent thickness. Wall‑thickness tolerance is ±5 %. Electrostatic Powder Coating All metal components will be cleaned of oil, dirt, and rust by sandblasting to create pores for better paint adhesion. Fine steel beads will be sprayed with compressed air to open pores and remove contaminants before coating. After manufacture, metal parts will be coated with polyester‑based electrostatic powder and cured in a 200‑220 °C oven for 20 minutes. Subsequently, parts will undergo a 10‑minute 70 °C dip in a 5 % degreasing bath, followed by a 15‑minute 50 °C dip in a 1 % iron bath. After rinsing and drying, the components will receive a durable polyester‑based outdoor powder coating, cured at 180‑200 °C for 20‑30 minutes. Weld seams will be fully coated after welding to prevent corrosion.