Classic Kids Playground
Price on request
SKU: SS-012582
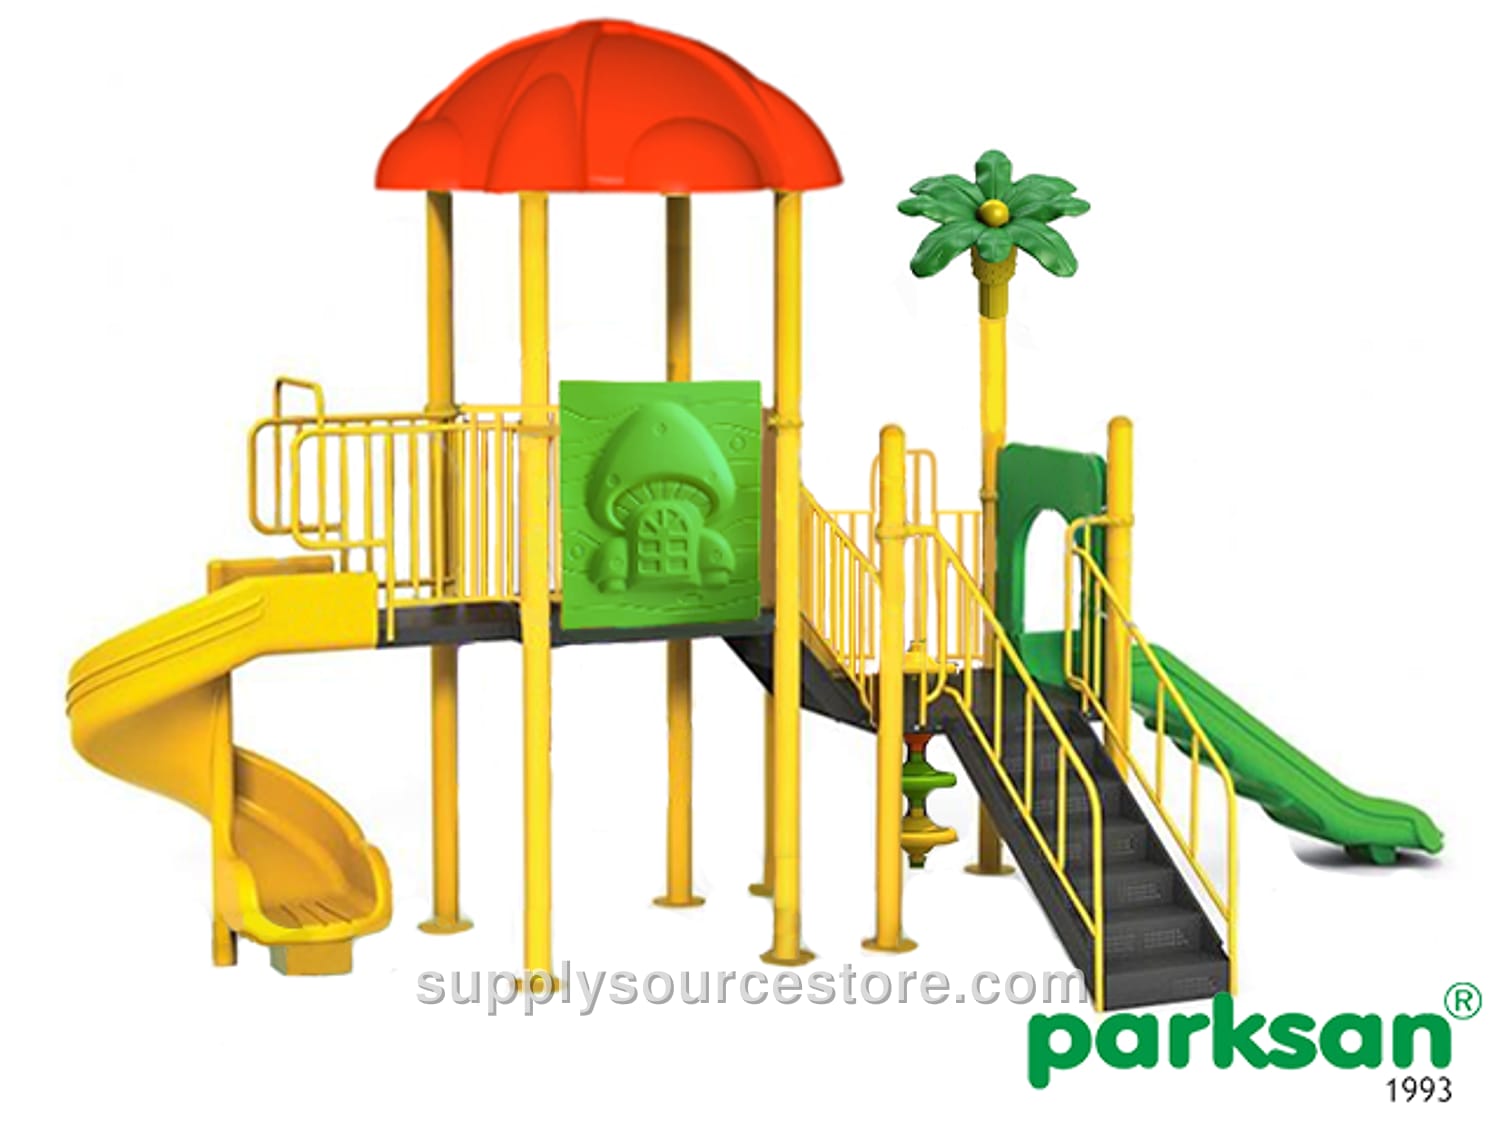
Product Technical Specifications Seat Area: 700 × 290 cm (276 x 114 in) Safety Area: 1100 × 690 cm (433 x 272 in) Slide Connection Height: 100 cm (39.4 in) – 150 cm (59.1 in) Age Group: 3 years and up Spare Parts: - Polyethylene roof – 1 piece (H: 100 cm (39.4 in)) - Polyethylene straight slide – 1 piece (H: 100 cm (39.4 in)) - Polyethylene spiral slide – 1 piece (H: 150 cm (59.1 in)) - Composite platform – 2 pieces (116 × 116 cm (45.7 x 45.7 in)) - Composite spiral‑extension platform – 1 piece (60 × 90 cm (23.6 x 35.4 in)) - Polyethylene slide barrier – 1 piece - Polyethylene platform barrier – 1 piece - Metal rail barrier – 1 piece - Composite stair – 1 piece - Stair railing – 1 piece (H: 100 cm (39.4 in)) - Wooden stair steps – 2 pieces (H: 50 cm (19.7 in)) - Stair with railing – 1 piece (H: 50 cm (19.7 in)) - Spiral‑extension platform metal railing – 1 piece - Tower – 8 pieces (4 × H: 150 cm (59.1 in), 4 × H: 100 cm (39.4 in)) - Polyethylene ‑tree figure – 1 piece - UFO climbing structure – 1 piece (H: 100 cm (39.4 in)) - Metal climbing entrance – 1 piece Polyethylene Products: Low‑density linear polyethylene (LLDPE) is a cost‑effective, durable thermoplastic. It offers good resistance to outdoor conditions and moisture, flexibility, modest mechanical strength, and excellent chemical resistance. It is used for slides, stairs, railings, barriers, accessories, roofs, and related components. Color‑fast pigments (lightfastness ≥ 6) are required to prevent fading. Load‑bearing parts must have a wall thickness of at least 6 mm (0.2 in); non‑load‑bearing barriers and shade structures require a minimum of 4 mm (0.2 in). Material distribution must be uniform to maintain consistent thickness. Dimensional tolerance is ±5 %. Carrier Construction: The carrier uses circular‑section steel tubes with a minimum diameter of 114 mm (4.5 in) and a wall thickness of at least 2 mm (0.1 in), cold‑formed to TS EN 10219‑2, TS‑6476, DIN 2394 standards, and joined by high‑frequency welding. Tubes are sandblasted and finished with a polyester‑based electrostatic powder coating. Electrostatic Powder Paint Process: All metal components are sandblasted to remove oil, grime, and rust, creating a porous surface for optimal paint adhesion. After sandblasting, fine powder particles are sprayed onto the parts with compressed air. The coating is then baked at 200‑220 °C for 20 minutes. Following fabrication, metal parts undergo a 10‑minute degreasing bath at 70 °C (5 % solution), a 15‑minute pickling bath at 50 °C (1 % solution), a final rinse and drying, and a cure in a 180‑200 °C oven for 20‑30 minutes. Weld seams are fully painted after welding to prevent corrosion.