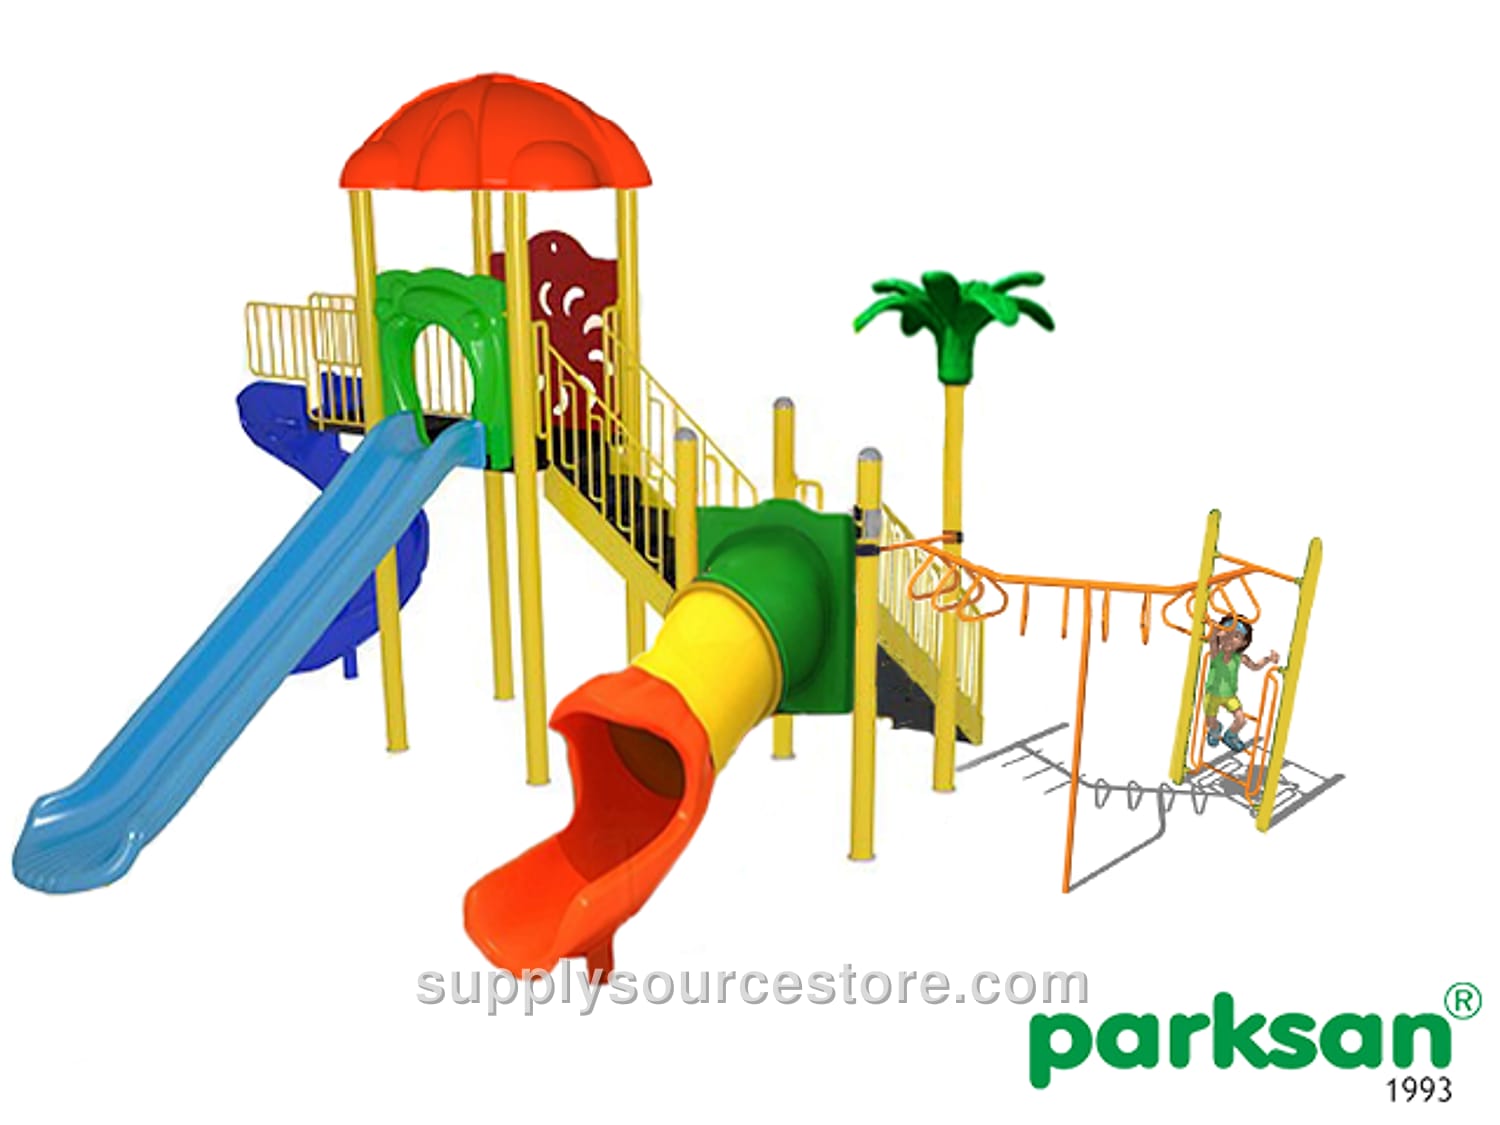
Classic Series Playground · SS-012575
Price on request
SKU: SS-012575
Product Technical Features Seating Area: 695 × 615 cm (274 x 242 in) Safety Area: 1095 × 1015 cm (431 x 400 in) Slide Connection Height: 100 cm (39.4 in) – 200 cm (78.7 in) Age Group: 3 + Years Spare Parts: - Polyethylene Roof – 1 piece (H: 100 cm (39.4 in)) - Tube Slide – 1 piece (H: 200 cm (78.7 in)) - Straight Slide – 1 piece (H: 200 cm (78.7 in)) - Spiral Slide – 1 piece - Composite Platform – 2 pieces (116 × 116 cm (45.7 x 45.7 in)) - Spiral Slide Extension – 1 piece - Polyethylene Slide Barrier – 2 pieces - Polyethylene Platform Barrier – 1 piece - Spiral Slide Metal Platform Railing – 1 piece - Composite Stairs – 2 pieces - Metal Stairs and Railing – 2 pieces - Tower – 4 pieces (H: 200 cm (78.7 in)) and 4 pieces (H: 100 cm (39.4 in)) - Commando Pull‑Up Bar Climbing – 1 piece - Polyethylene Figure – 1 piece Polyethylene Products: Low‑density linear polyethylene (LLDPE) is a thermoplastic used in many products. It is semi‑permeable, soft, and highly durable; its low cost and high resistance make it popular in industry. Mechanical properties depend on molecular weight, crystal structure and branch type. To prevent color fading, masterbatch pigments must have a light‑fastness value of 6 or higher. Material thickness must be at least 6 mm (0.2 in) at points subjected to pressure and friction, and at least 4 mm (0.2 in) for barriers and shading components that are not pressure‑exposed. Thickness uniformity is required, with overall dimensional tolerances of ±5 %. Carrier Construction: Minimum‑diameter steel tubes of 114 mm (4.5 in) with at least 2 mm (0.1 in) wall thickness, compliant with TS EN 10219‑2, TS‑6476 and DIN 2394, are cold‑formed and welded by high‑frequency welding. Tubes are powder‑coated using a polyester‑based electrostatic process after sandblasting. Electrostatic Powder Coating: All metal parts are sandblasted to remove oil, dirt and rust, creating a porous surface for better paint adhesion. Fine steel shot is sprayed under pressure to open pores and clear contaminants. After sandblasting, components receive a polyester‑based electrostatic powder coat and are baked in a 200‑220 °C oven for 20 minutes. Following metal fabrication, parts undergo a 10‑minute, 70 °C oil‑removal bath (5 % solution), then a 15‑minute, 50 °C iron‑dip bath (1 % solution), followed by rinsing and drying. The entire assembly is then painted with a durable polyester‑based powder in an outdoor‑rated electrostatic system and cured in a 180‑200 °C oven for 20‑30 minutes. Welding seams are fully covered with a continuous coat to prevent corrosion.