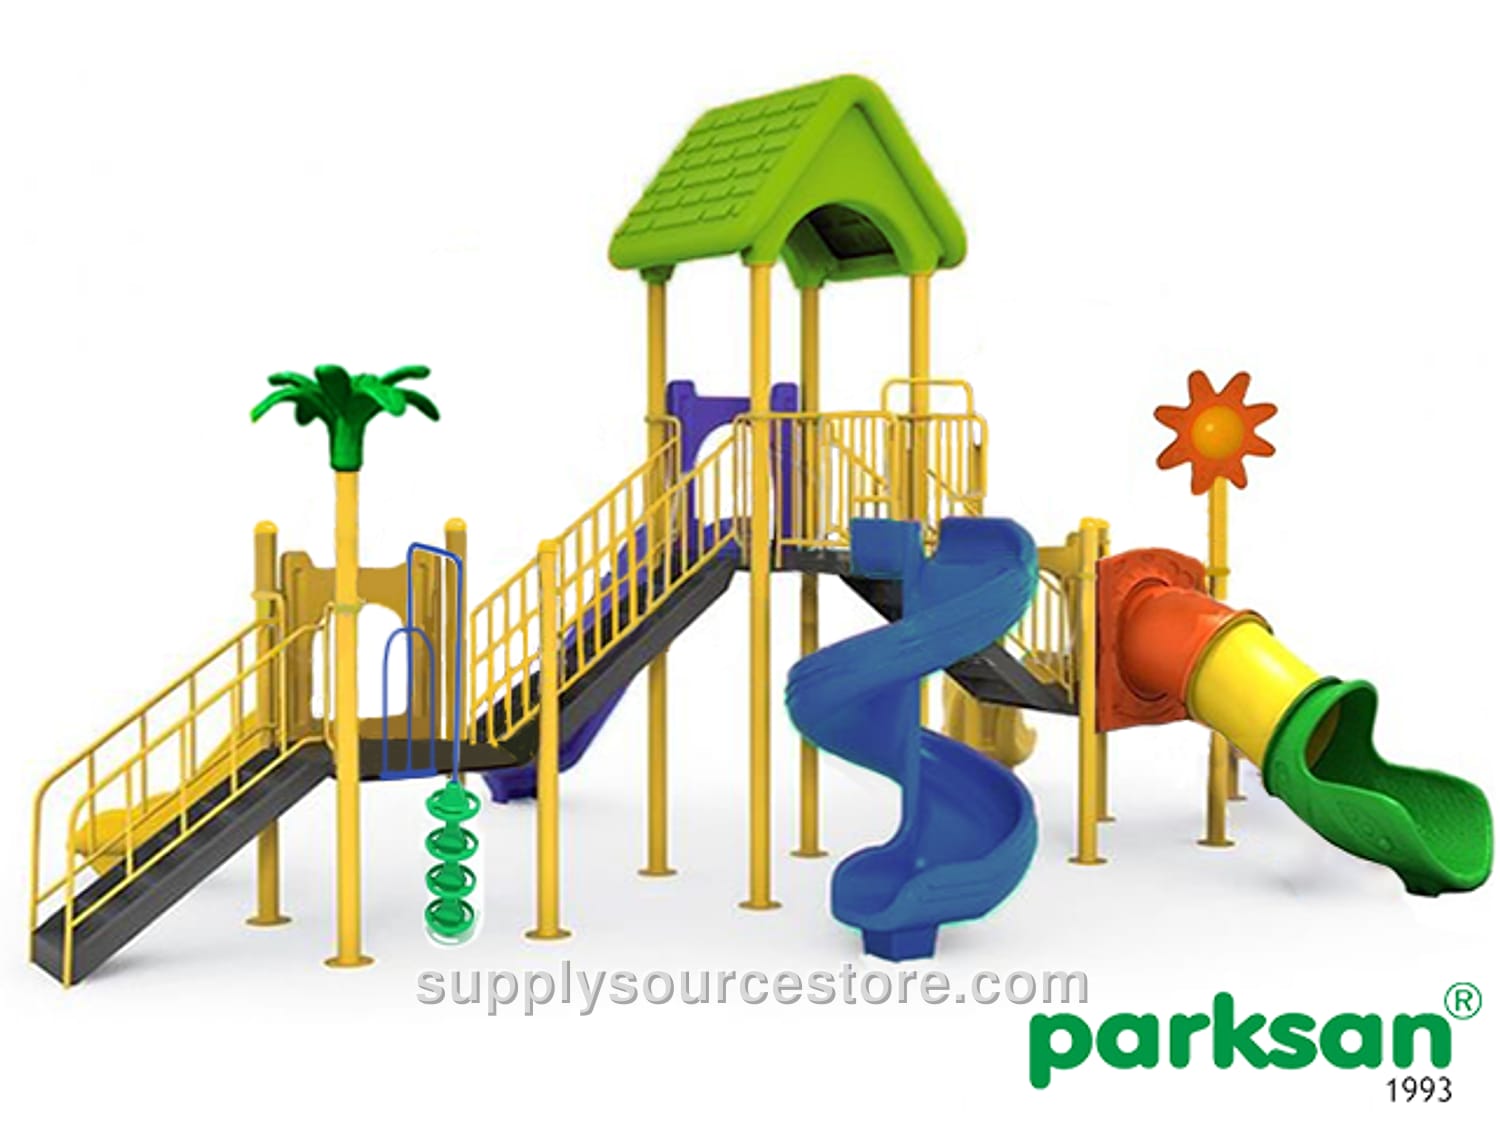
Classic Series Children's Playground · SS-012572
Price on request
SKU: SS-012572
Technical specifications: Seating area 725 × 630 cm (285 x 248 in); safety area 1125 × 1030 cm (443 x 406 in); slide mounting height 100–200 cm (39.4-78.7 in); suitable for children 3 years and up. Spare parts include: - Polyethylene roof – 1 piece - Dual straight slides, H 100 cm (39.4 in) – 1 piece - Tube slide, H 100 cm (39.4 in) – 1 piece - Right‑inclined slide, H 100 cm (39.4 in) – 1 piece - Straight slide, H 200 cm (78.7 in) – 1 piece - Spiral slide, H 200 cm (78.7 in) – 1 piece - Composite platform 116 × 116 cm (45.7 x 45.7 in) – 3 pieces - Spiral slide extension – 1 piece - Polyethylene slide barriers – 4 pieces - Spiral slide metal platform guard – 1 piece - Composite stairs – 3 pieces - Stair guard – 3 pieces - Tower, H 200 cm (78.7 in) – 4 pieces - Tower, H 100 cm (39.4 in) – 8 pieces - UFO climbing unit, H 100 cm (39.4 in) – 1 piece - Metal climbing entrance – 1 piece - Polyethylene mushroom figure – 1 piece - Polyethylene figure – 1 piece Polyethylene components are made from low‑density linear polyethylene (LLDPE), a semi‑permeable, flexible and highly durable thermoplastic. It provides good resistance to outdoor conditions, moisture and chemicals. Color pigments must have a light‑fastness rating of 6 or higher. Wall thickness is at least 6 mm (0.2 in) for parts that bear pressure or friction and at least 4 mm (0.2 in) for non‑load‑bearing barriers, with a tolerance of ±5 %. Carrier construction: Steel tubes with a minimum outer diameter of 114 mm (4.5 in) and wall thickness of ≥2 mm (0.1 in) are cold‑formed to TS EN 10219‑2, TS‑6476 and DIN 2394, then welded by high‑frequency welding. Tubes are sand‑blasted and coated with a polyester‑based electrostatic powder paint. Electrostatic powder coating: All metal parts are sand‑blasted to remove oil, dirt and rust, creating a porous surface for better adhesion. Fine steel beads are sprayed with pressurized air to open pores. After coating with polyester‑based powder, parts are cured in a 200–220 °C oven for 20 minutes, then undergo a 10‑minute oil‑removal bath at 70 °C (5 % solution), followed by a 15‑minute iron‑pickling bath at 50 °C (1 % solution). After rinsing and drying, the components are baked again at 180–200 °C for 20–30 minutes. All welds are fully painted to prevent corrosion.