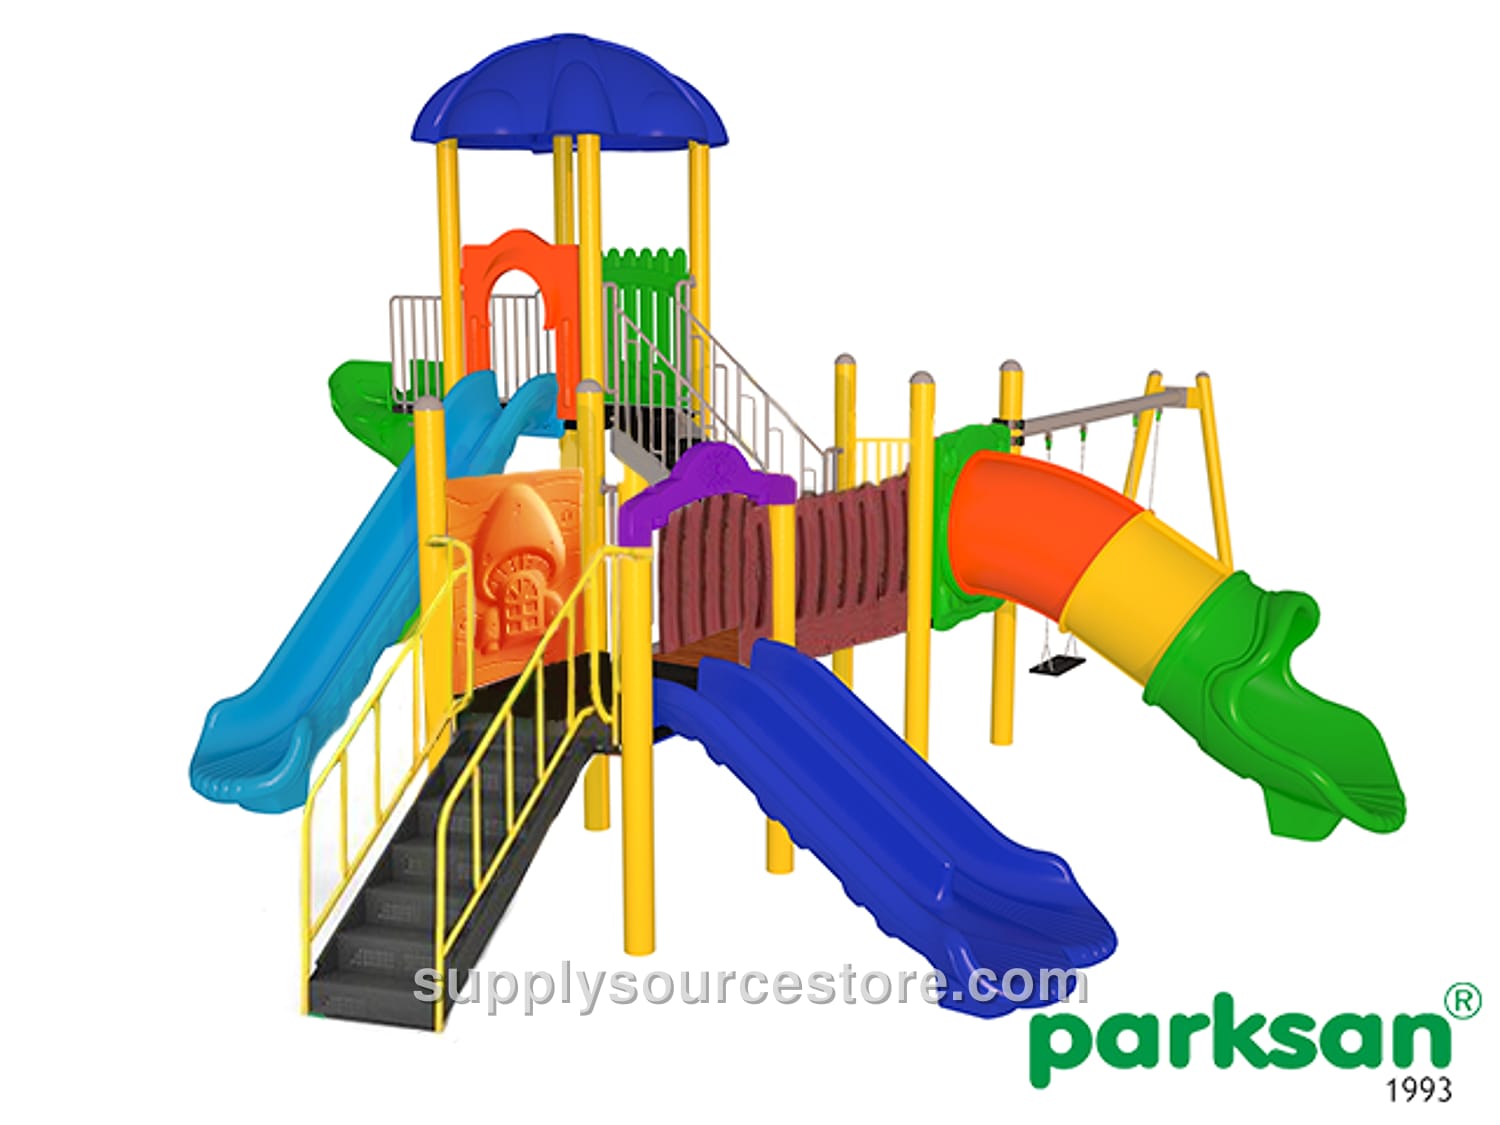
Classic Series Playground · SS-012571
Price on request
SKU: SS-012571
Technical specifications: Seating area 800 × 815 cm (315 x 321 in); safety area 1200 × 1215 cm (472 x 478 in); slide connection height 100–200 cm (39.4-78.7 in); suitable for children 3 years and up. Spare parts include: - Polyethylene roof – 1 piece - Double straight slide, H 100 cm (39.4 in) – 1 piece - Tube slide, H 100 cm (39.4 in) – 1 piece - Straight slide, H 200 cm (78.7 in) – 1 piece - Spiral slide, H 200 cm (78.7 in) – 1 piece - Composite platform 116 × 116 cm (45.7 x 45.7 in) – 3 pieces - Spiral slide extension – 1 piece - Polyethylene slide barrier – 2 pieces - Polyethylene slide belt – 1 piece - Polyethylene platform barrier – 2 pieces - Metal platform barrier – 1 piece - Polyethylene bridge – 1 piece - Spiral slide metal platform guard – 1 piece - Composite stair – 2 pieces - Metal stair guard – 2 pieces - Tower, H 200 cm (78.7 in) – 4 pieces - Tower, H 100 cm (39.4 in) – 8 pieces - Swing A – 2 pieces - Swing support – 1 piece - Chain‑linked polyethylene guarded swing seat – 1 piece - Chain‑linked rubber swing seat – 1 piece Polyethylene components are made from low‑density linear polyethylene (LLDPE), a semi‑permeable, easily softened and highly durable thermoplastic. It offers excellent resistance to outdoor conditions, moisture and chemicals. Color pigments must have a light‑fastness rating of 6 or higher. Edge thickness is at least 6 mm (0.2 in) for load‑bearing parts and at least 4 mm (0.2 in) for non‑load‑bearing barriers, with a tolerance of ±5 %. Carrier construction: The carrier structure consists of circular‑section steel pipes fabricated to TS EN 10219‑2, TS‑6476 and DIN 2394 standards by cold forming, with a minimum wall thickness of 2 mm (0.1 in) and a minimum diameter of 114 mm (4.5 in). Pipes are welded with high‑frequency welding and coated with a polyester‑based electrostatic powder finish applied after sandblasting. Electrostatic powder paint: All metal parts are blasted to remove oil, grime and rust, then prepared for coating. A fine‑grain abrasive creates pores for better paint adhesion. After blasting, parts are sprayed with a polyester‑based electrostatic powder and cured in a 200–220 °C oven for 20 minutes. They then undergo a 10‑minute degreasing bath at 70 °C (5 % solution) followed by a 15‑minute phosphating bath at 50 °C (1 % solution). After a final rinse and drying, the components are baked again at 180–200 °C for 20–30 minutes. Weld seams are fully covered with a continuous powder coat to prevent corrosion.