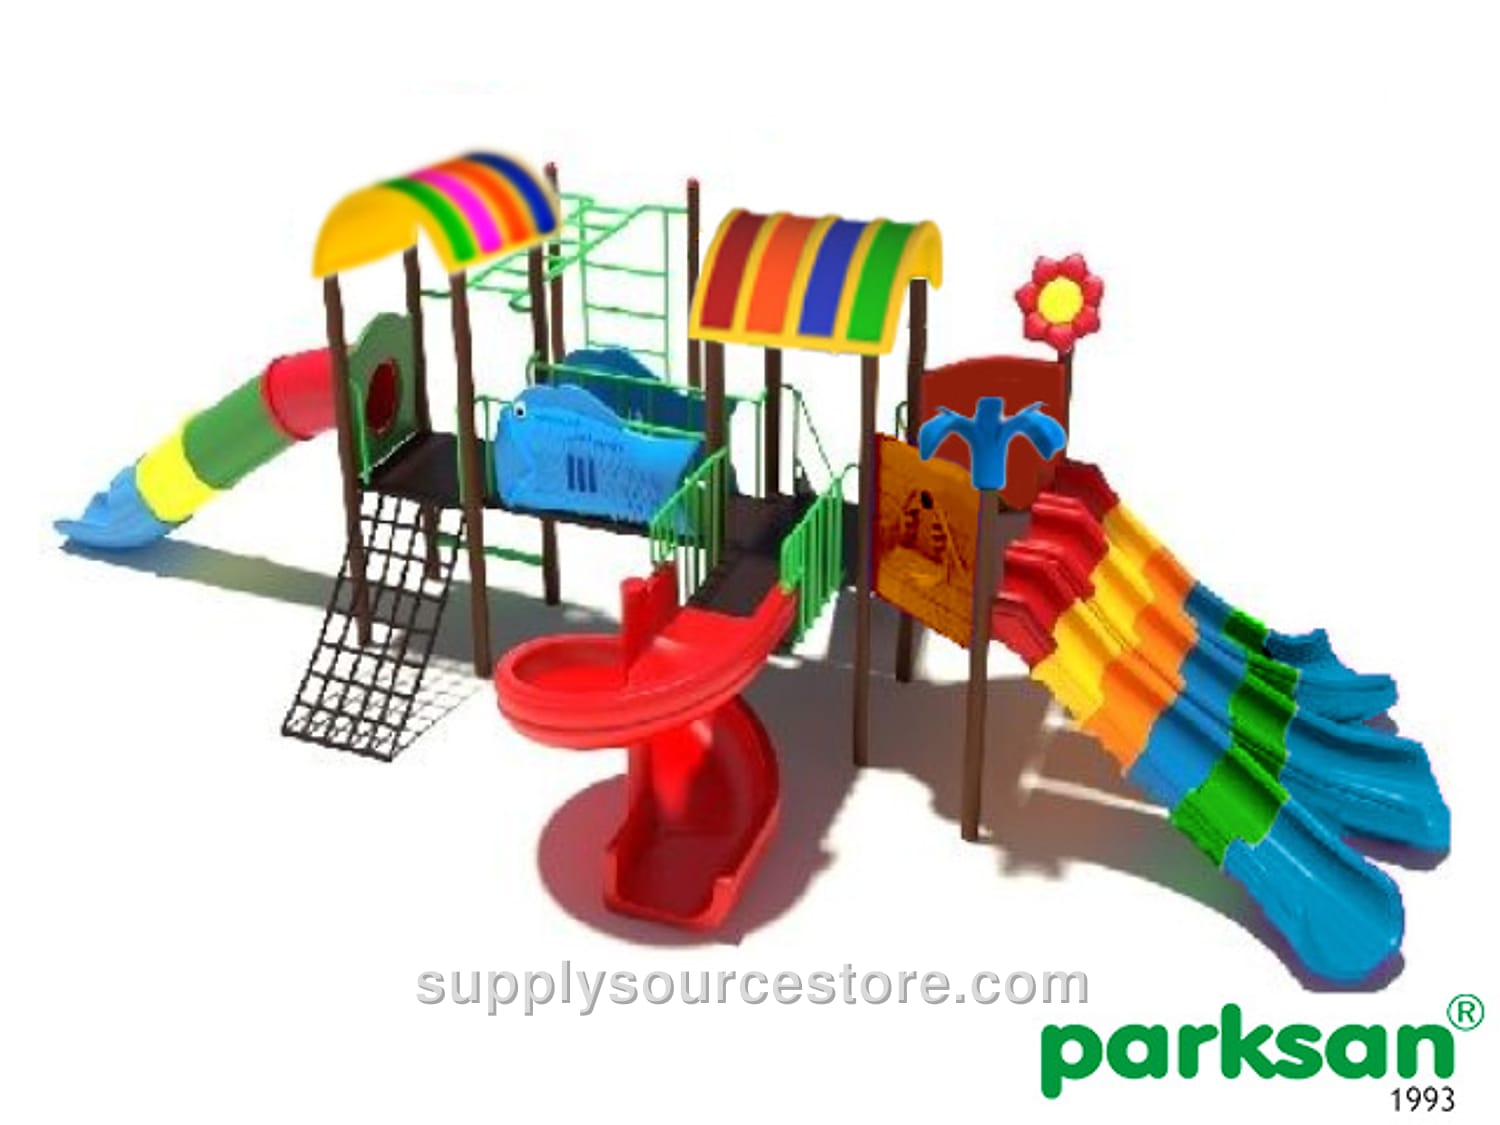
Rainbow Series Children’s Playground
Price on request
SKU: SS-012556
Spare parts for the Rainbow Series Children’s Playground: - 1 × 150 cm (0.4 x 59.1 in) metal guardrail (H) - 1 × composite stair - 3 × 116 × 116 mm (0.1 x 4.6 x 4.6 in) composite square platforms - 2 × 116 × 116 mm (0.1 x 4.6 x 4.6 in) composite triangular platforms - 1 × metal bridge extension - 1 × polyethylene fish tunnel - 1 × 150 cm (0.4 x 59.1 in) rope‑climbing element (H) - 1 × 150 cm (0.4 x 59.1 in) tube slide (H) - 1 × 150 cm (0.4 x 59.1 in) triple slide (H) - 1 × pull‑up bar - 1 × spiral slide extension - 1 × 150 cm (0.4 x 59.1 in) spiral slide (H) - 1 × rainbow roof - 2 × polyethylene canopy barriers - 1 × polyethylene slide entrance - 1 × polyethylene flower figure - 1 × polyethylene figure - 10 × 150 cm (3.9 x 59.1 in) tower Polyethylene Products: Low‑density linear polyethylene (LLDPE) is a thermoplastic used in many applications. It is semi‑permeable, flexible, and highly durable, offering low cost and strong resistance. Depending on density and chemical characteristics, polyethylene is classified into several categories. Its mechanical properties are affected by molecular weight, crystallinity, and branching type. Generally it provides good outdoor and moisture resistance, flexibility, modest mechanical strength, and excellent chemical resistance. Polyethylene components are used to make slides, stairs, guardrails, barriers, accessories, roofs, and more. To prevent color fading, masterbatch pigments must have a light‑fastness rating of 6 or higher. Material thickness at pressure‑ and friction‑exposed points must be at least 6 mm (0.2 in); barrier or shade items that do not bear pressure require a minimum of 4 mm (0.2 in). Thickness should be uniform across the part. Product thickness and dimensional tolerances are ±5 %. Electrostatic Powder Coating: All metal parts are grit‑blasted to remove oils, dirt, and rust, creating a porous surface for better paint adhesion. Fine steel shot is propelled with compressed air to open pores and clean the metal. After fabrication, metal components are coated with a polyester‑based electrostatic powder and cured in a 200–220 °C oven for 20 minutes. Parts then receive a 10‑minute dip at 70 °C in a 5 % degreasing bath, followed by a 15‑minute dip at 50 °C in a 1 % iron pickling bath. After rinsing and drying, the components are coated with a durable polyester‑based outdoor powder finish, cured at 180–200 °C for 20–30 minutes. Weld seams are fully coated after welding to prevent corrosion.