Children's Playground (Afacan Series) · SS-012293
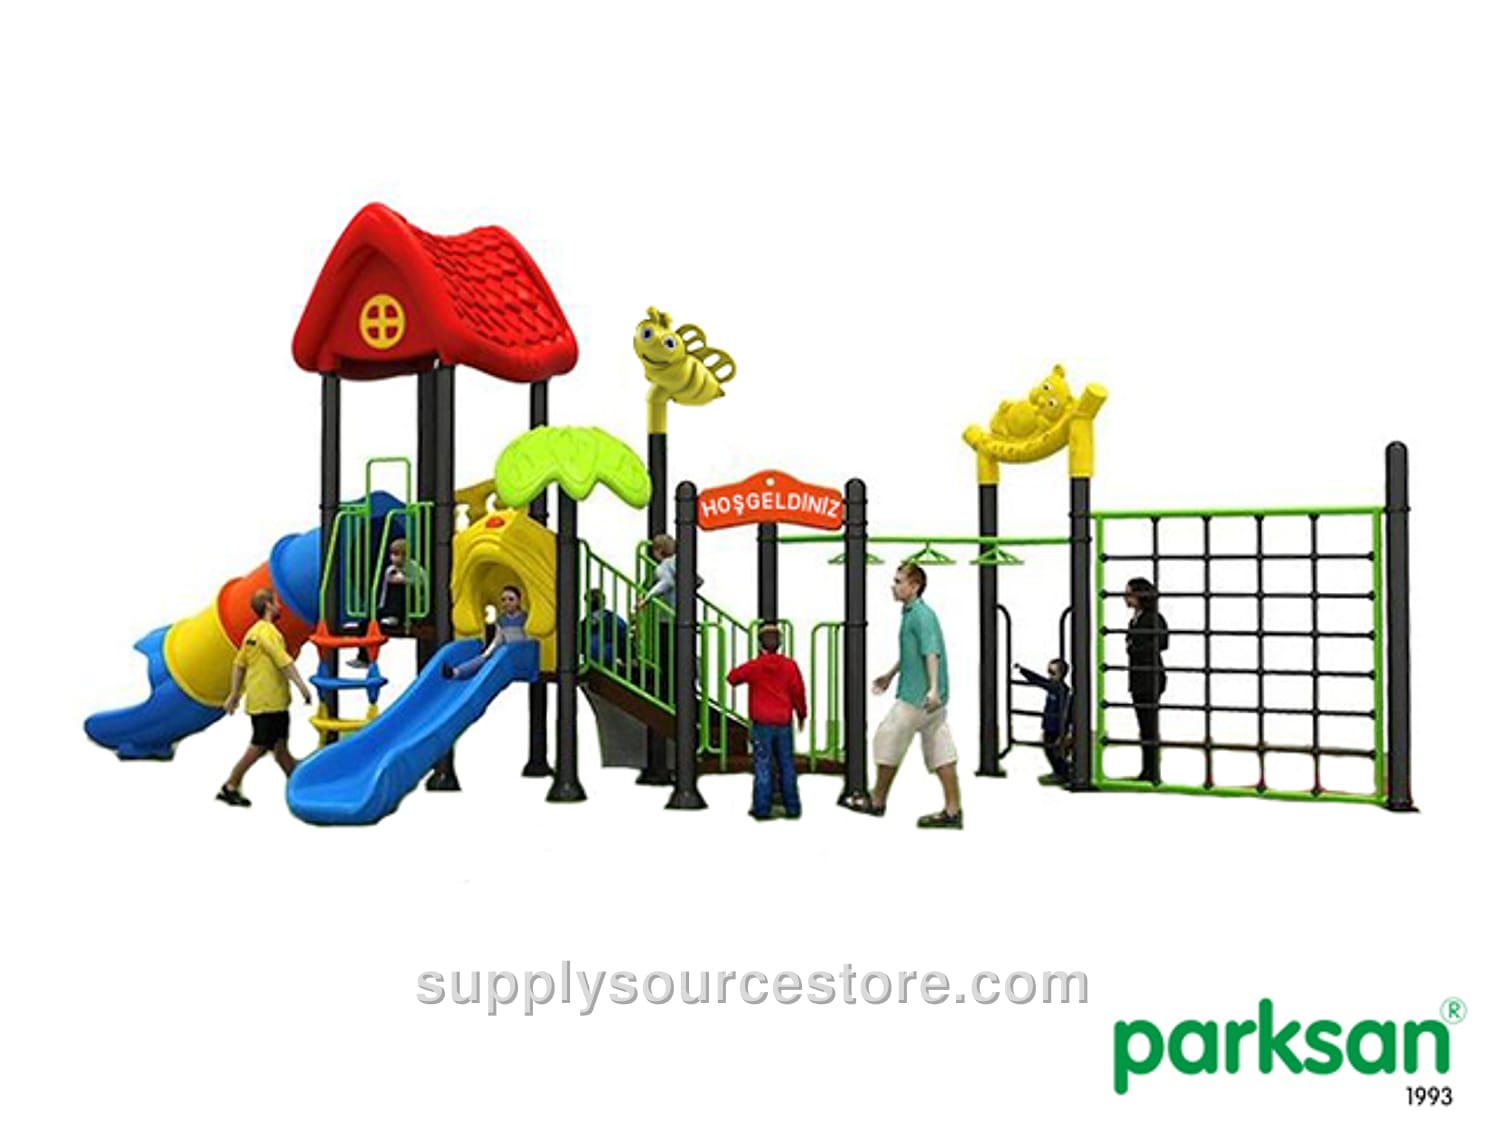
Price on request
SKU: SS-012293
Polyethylene Products Low‑density or linear low‑density polyethylene (LLDPE) is a thermoplastic used in various products. It is a semi‑permeable, flexible, and highly durable polymer. Its low cost and high resistance make it popular in industry. Polyethylene is classified into categories based on density and chemical properties. Mechanical properties depend on molecular weight, crystal structure, and branching type. While properties vary by type, general characteristics include good resistance to outdoor conditions and moisture, flexibility, low mechanical strength, and excellent chemical resistance. Polyethylene products are used to manufacture slides, stairs, railings, barriers, accessories, roofs, etc. To prevent color fading, masterbatch pigments used to color polyethylene must have a light‑fastness rating of 6 or higher. The product wall thickness must be at least 6 mm (0.2 in) for areas exposed to pressure and friction, and at least 4 mm (0.2 in) for barriers and shading elements not subject to pressure. Material distribution must be uniform, creating consistent thickness. Wall thicknesses and dimensional tolerances are ±5 %. Carrier Construction The carrier construction consists of circular steel tubes with a minimum outer diameter of 114 mm (4.5 in) and a minimum wall thickness of 2 mm (0.1 in), cold‑formed according to TS EN 10219‑2, TS‑6476, DIN 2394 standards and welded by high‑frequency welding. Tubes are painted by sandblasting followed by a polyester‑based electrostatic powder coating. Electrostatic Powder Coating All metal parts are first cleaned by sandblasting to remove oil, dirt, and rust, creating a porous surface for better paint adhesion. Fine steel shot is then sprayed with compressed air to open additional pores and remove contaminants. After fabrication, metal components are coated with a polyester‑based electrostatic powder and cured in a 200–220 °C oven for 20 minutes. Subsequently, they undergo a 10‑minute dip in a 70 °C, 5 % concentration degreasing bath, followed by a 15‑minute dip in a 50 °C, 1 % concentration iron bath. After rinsing and drying, the parts are painted with a durable polyester powder coating and cured at 180–200 °C for 20–30 minutes. Weld seams are completely painted after welding to prevent corrosion.