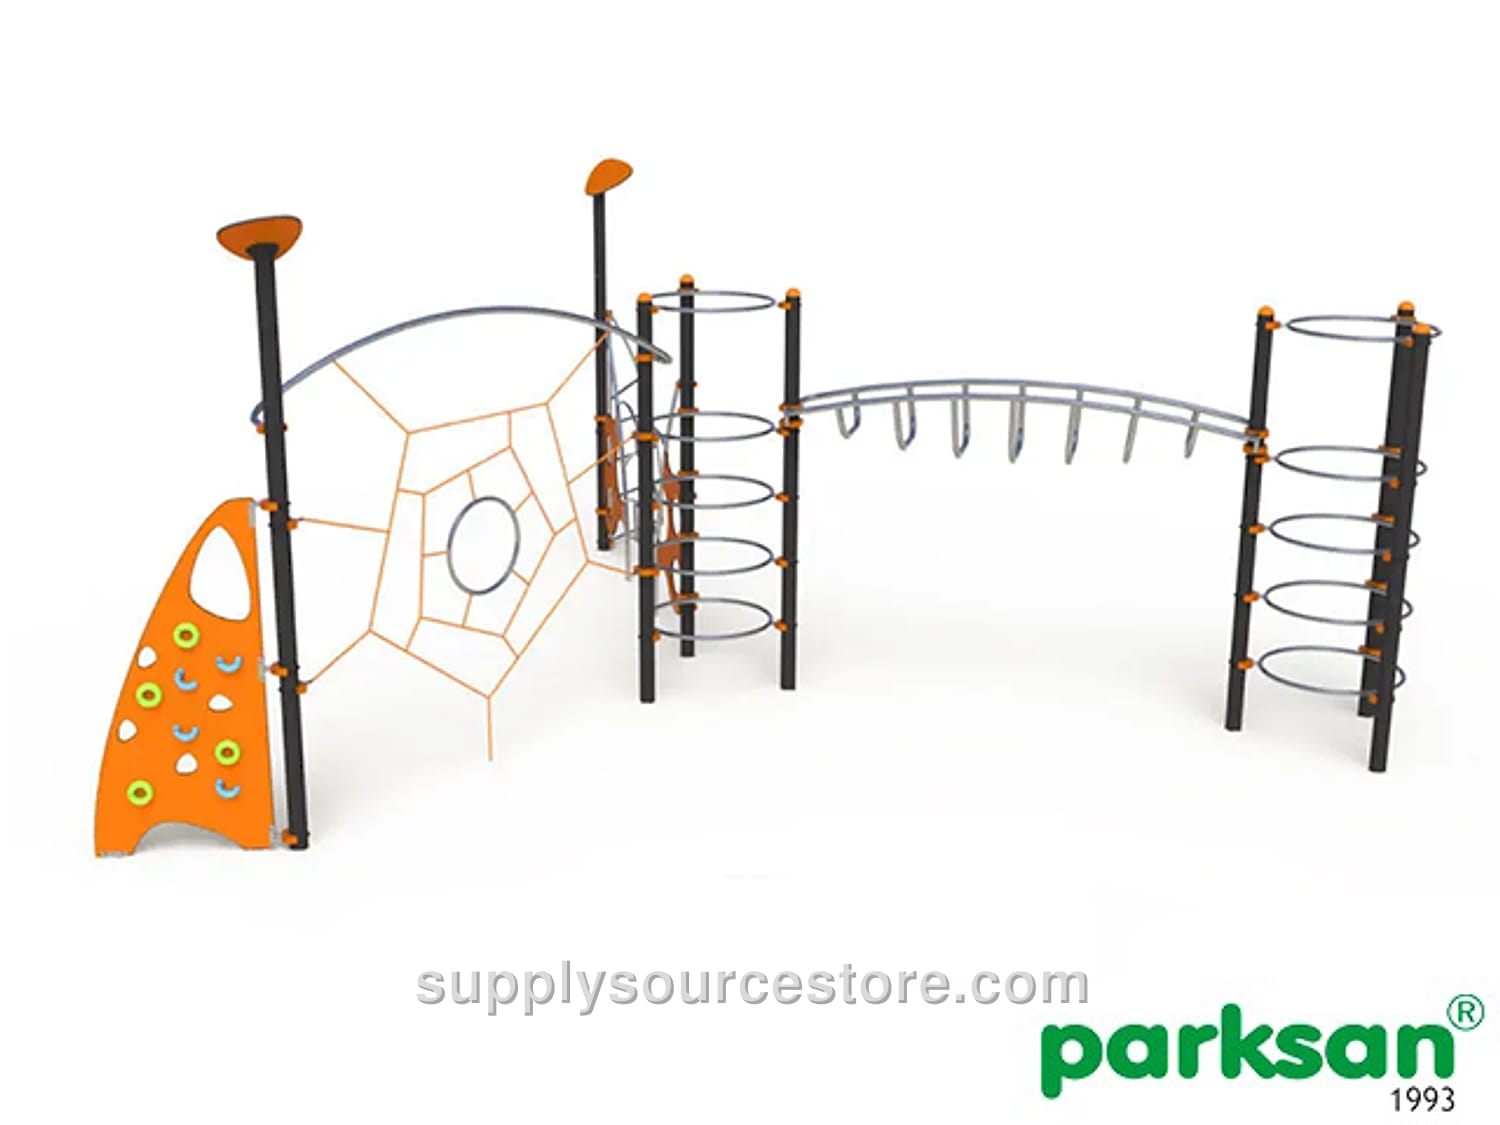
Next Generation Kids Playground Play Set · SS-012089
Price on request
SKU: SS-012089
Product Technical Specifications Age Group: 5+ Usage Area: 610x430 cm (240 x 169 in) Safety Area: 614×434 cm (242 x 171 in) Spare Parts H:245cm (96.5 in) Rope Rock Climbing Unit – 1 piece H:245cm (96.5 in) Rope Straight Climbing Unit – 1 piece H:245cm (96.5 in) Pentagonal Net Climbing Element – 1 piece H:245cm (96.5 in) Passage Climbing Element – 2 pieces H:245cm (96.5 in) Straight Trapezoid Circular Step – 1 piece H:245cm (96.5 in) Metal‑HDPE Butterfly Model Climbing Unit – 1 piece Polyethylene Products Low‑density linear polyethylene (LLDPE – Linear Low Density Polyethylene) is a thermoplastic used in various products. It is a semi‑permeable, softening‑able, and highly durable polymer. Its low cost and high resistance make it popular in industry. Polyethylene is classified into categories based on density and chemical properties. Mechanical properties depend on molecular weight, crystalline structure, and branching type. Although properties vary by type, it generally offers good resistance to outdoor conditions and moisture, flexibility, low mechanical strength, and excellent chemical resistance. Polyethylene products are used in the manufacture of slides, stairs, railings, barriers, accessories, roofs, etc. To prevent color fading, masterbatch pigments used to color polyethylene must have a lightfastness rating of 6 or higher. The material thickness should be a minimum of 6 mm (0.2 in) for components exposed to pressure and friction, and a minimum of 4 mm (0.2 in) for barriers and shading items not subjected to pressure. Material distribution must be uniform to achieve consistent thickness. Product thickness and dimensional tolerance are ±5%. Electrostatic Powder Coating All metal parts will be prepared for coating by sandblasting to remove oils, dirt, and rust, creating pores for better paint adhesion. Fine steel beads are sprayed with pressurized air to open pores and remove contaminants before coating. After fabrication, metal components are coated with a polyester‑based electrostatic powder and baked in a 200‑220 °C oven for 20 minutes. Subsequently, components undergo a 10‑minute 70 °C dip in a 5% oil‑removal bath, followed by a 15‑minute 50 °C dip in a 1% iron bath. After rinsing and drying, the material is coated with a durable outdoor polyester‑based powder and baked at 180‑200 °C for 20‑30 minutes. Weld seams are painted after welding to prevent corrosion, and the entire product is finished as a single piece.